A complete hot-press cycle
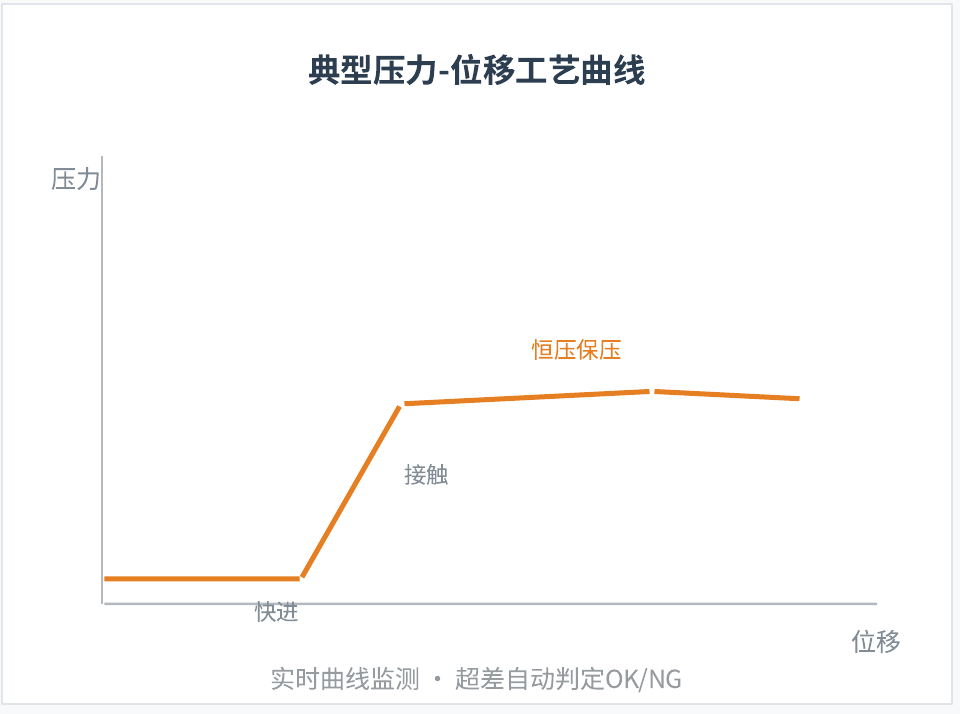
Rapid approach → slow contact → constant-force dwell → cooling delay → return. Reduce speed at contact, coordinate temperature and dwell during forming, and adjust cooling for material and release behavior. Establish settings through part trials.
- 01Rapid approach
- 02Slow contact
- 03Force dwell
- 04Cooling delay
- 05Return
Illustrative sequence; validate targets, speed, time and evaluation criteria for the part.
 View full image ⤢
The source curve illustrates pressure variation through the process. It is not a production measurement or a force, stroke or accuracy specification. Assess actual trials using position, temperature, dwell and cooling records together.
Image source:Benchtop hot-press introduction · p.7Limits of the benchtop specification
This product introduction specifies 50–350°C, temperature-control error ≤±2°C and positioning repeatability ±0.01 mm, with a Type K thermocouple, PID control and PTFE non-stick tooling. Control error is not platen temperature uniformity. The general hot-press brochure describes a separate configuration; its 0–300°C and ±1°C figures must not be combined with this model.
 View full image ⤢
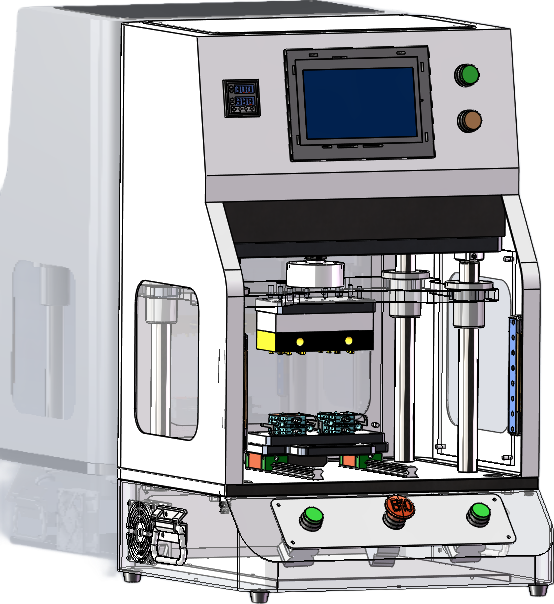
The design illustration shows four-column guidance, the heated work area and a transparent guard. The product introduction specifies a Type K thermocouple, PID control and a PTFE non-stick surface. Validate head shape, support, heated area and release with actual stakes or bonded parts.
Image source:Benchtop hot-press introduction · pp.4–6 · design illustrationValidate materials and tooling together
The introduction lists ABS, PC, glass-reinforced PA and PP heat staking, plus FPC and insulation bonding. Supply material grades, stake dimensions, heated area, appearance criteria and pull-out requirements. Validate tool shape, support, non-stick surface, release and cooling. A material name alone cannot define the process window.
Quotation & acceptance checklist
Confirm pressing force, stroke, table and daylight dimensions, power supply, heating zones and cycle time; the supplied introduction does not specify universal values for these items. Acceptance should cover part strength and appearance, temperature measurement locations and stabilization, force/position repeatability, recipe recall, USB export and actual operation of two-hand start, guard, emergency stop and limits.